Last updated: October 2026
By Ron, Sputtek
Manufacturers rarely need a coating simply because a part is old. They need a repeatable way to address a specific failure: galling on a stamping die, sticking in a mold, edge wear on a cutting tool, soldering in die casting, or erosion on a shaft. Industrial coatings services are most valuable when they connect that failure to a surface treatment, a controlled preparation sequence, and measurable acceptance criteria.
Sputtek provides PVD, DLC, Thermospray, and pulsed HVOF services from a 15,000-square-foot facility in the Greater Toronto Area. Its capabilities cover preparation, deposition, finishing, and quality control, allowing a project to move from prototype assessment to production processing with the same engineering focus.
What industrial coatings services include
Industrial coatings services are not limited to putting material on a part. They normally include application engineering, cleaning, masking, fixturing, deposition, inspection, and – when required – stripping, lapping, polishing, or dimensional finishing. Each stage affects whether the coating adheres, remains uniform, and performs on the actual production surface.
Thin-film PVD and DLC coatings modify the outermost surface while adding only a small amount of material. Thermal spray processes, including HVOF, are used when a project needs a thicker and tougher layer that can resist impact, erosion, or wear and may also restore a worn dimension.
- Application review: the supplier examines the substrate, failure mode, operating environment, geometry, and production requirements.
- Preparation: cleaning, blasting, microblasting, masking, and fixturing create the conditions needed for adhesion and uniform coverage.
- Coating: the selected process deposits a ceramic, carbon-based, carbide, metallic, or composite layer suited to the duty cycle.
- Finishing: lapping or polishing can return a coated surface to its required finish, fit, or release condition.
- Verification: thickness, adhesion, hardness, surface finish, and traceability records provide evidence that the process met the agreed specification.
For background on the vacuum process, this PVD coating guide explains the role of energy, targets, and substrate preparation. A useful service program should translate that technical knowledge into decisions about your parts rather than offer a coating name without an application rationale.
PVD and DLC versus Thermospray and pulsed HVOF
The central selection question is whether the part needs a thin functional film or a thicker wear surface. PVD and DLC preserve precision geometry and are often selected for tools, dies, molds, and components where friction, hardness, release, or sticking is the main concern. Thermospray and pulsed HVOF are better suited to parts that need a substantial overlay for abrasion, erosion, impact, or dimensional rebuilding.
| Decision factor | PVD or DLC | Thermospray or pulsed HVOF |
|---|---|---|
| Layer role | Thin functional surface film | Thick protective or restorative overlay |
| Typical application | Cutting tools, dies, molds, punches, precision components | Shafts, sleeves, rollers, heavy wear surfaces, rebuilt diameters |
| Primary mechanisms | Hardness, lower friction, release, reduced adhesion | Abrasion, erosion, impact resistance, wear protection, recovery of dimensions |
| Geometry consideration | Useful where tight tolerances must be preserved | Requires allowance for buildup and post-coating finishing |
| Preparation priority | Cleanliness, substrate condition, masking, and line-of-sight | Surface profile, bond preparation, spray angle, masking, and finishing allowance |
These categories are not interchangeable. A thin PVD film is not a substitute for a thick rebuild layer on a damaged shaft, and a thermal-spray overlay may be unnecessary when the problem is release or galling on a precision mold surface. The correct process is the one that addresses the dominant failure without creating a new tolerance, finish, or thermal problem.
When PVD or DLC is the better choice
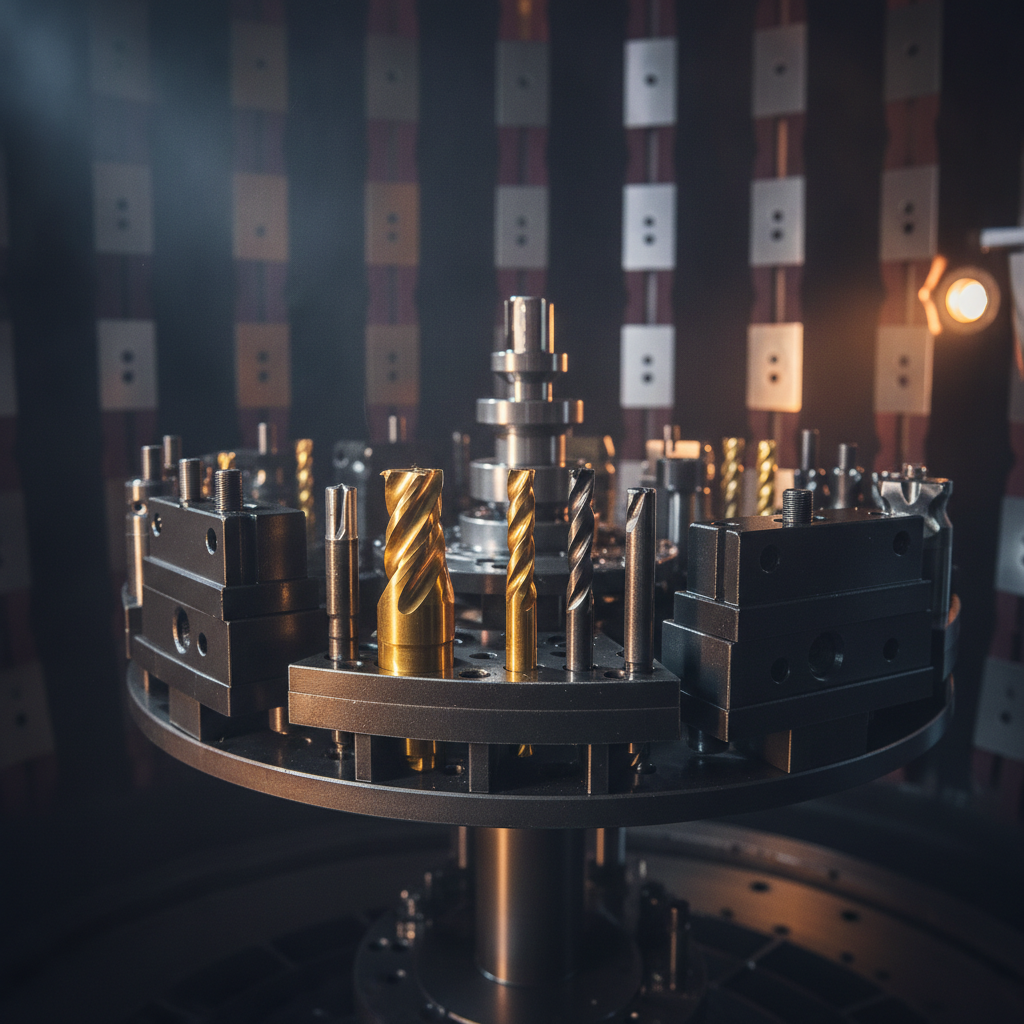
PVD coating services deposit a hard film in a vacuum environment. Common coating families include TiN, TiCN, AlTiN, CrN, and DLC, although the appropriate chemistry depends on the substrate, temperature, counterface, lubricant, material being processed, and failure mechanism. The coating name alone does not establish suitability.
PVD and DLC are often considered when the part must retain close geometry while gaining a harder, lower-friction, or less adhesive surface. They can be useful on cutting tools, stamping dies, injection molds, punches, shutoffs, and precision components. In machining, the objective may be improved edge retention or reduced built-up edge. In molding, it may be cleaner release, less sticking, or better resistance to wear on gates and shutoffs.
Questions to answer before selecting a thin film
- What material contacts the coated surface, and is the contact sliding, cutting, forming, or impact-based?
- Is the failure caused mainly by abrasion, adhesive pickup, corrosion, heat, or material transfer?
- Which surfaces must remain uncoated, and what masking or fixturing will protect them?
- Can the geometry be exposed consistently during deposition?
- Will the finished coating need polishing or lapping to meet a release, sealing, or surface-finish requirement?
DLC is generally considered where low friction and reduced adhesion are important, but it still requires a compatible substrate and preparation sequence. The supplier should assess the complete contact system rather than promise that a carbon-based film will solve every wear problem.
For a broader explanation of the process and terminology, see this complete PVD coating guide. If you are comparing suppliers, a PVD companies evaluation guide can help organize questions about equipment, preparation, inspection, and production capacity.
When Thermospray or pulsed HVOF is the better choice
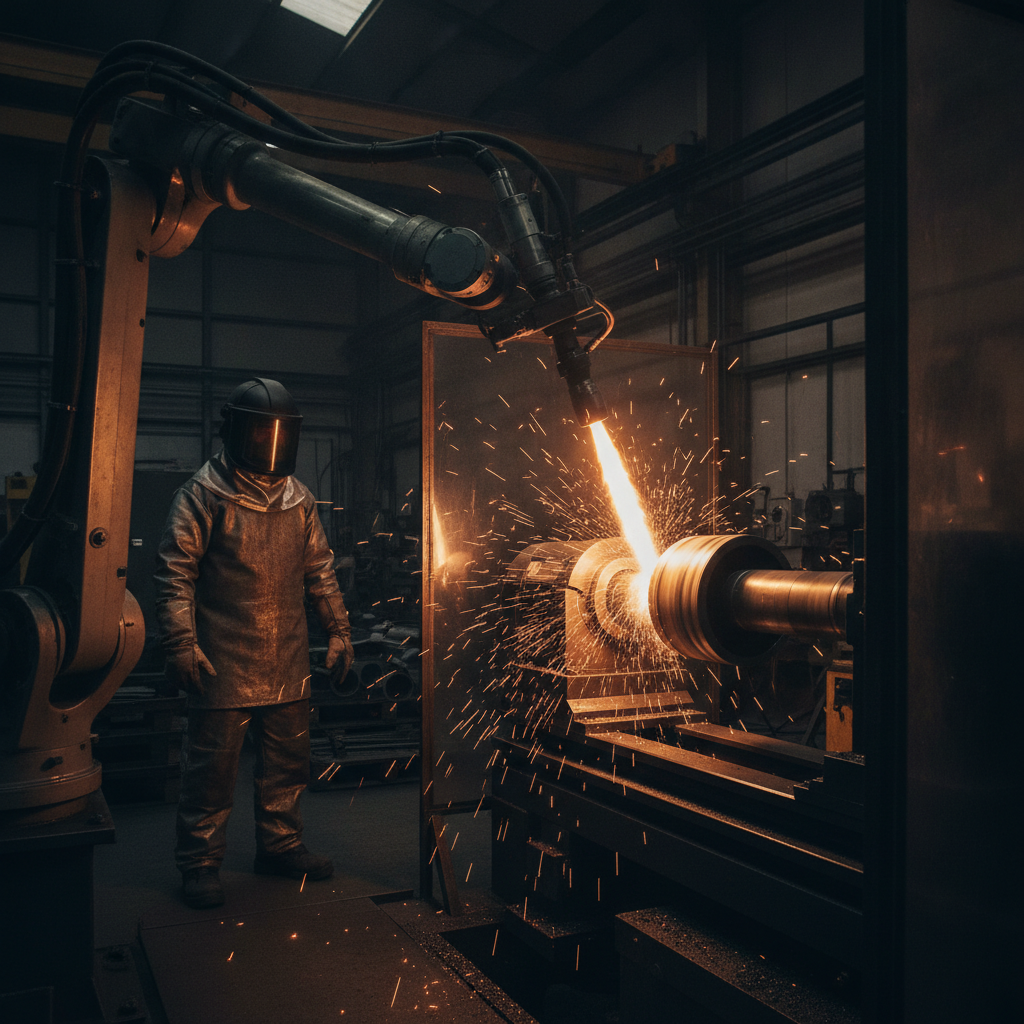
Thermospray and pulsed HVOF apply particles at high velocity to build a dense coating. These processes are considered when a part faces substantial abrasion, erosion, impact, or dimensional wear, or when a worn surface needs to be restored before final machining. Carbides, metals, and cermet-type materials can be selected according to the environment and required wear mechanism.
Typical candidates include shafts, sleeves, rollers, pins, and other components with larger working surfaces. A coating engineer must account for the original dimension, the amount of buildup required, the final machining route, substrate temperature, masking, and the way the part will be loaded in service.
Thermal-spray planning points
- Allowances: provide enough material for finishing without assuming that more thickness automatically means longer life.
- Surface profile: specify cleaning and roughening requirements that support mechanical bonding and consistent coverage.
- Access: confirm that the spray path can reach internal diameters, shoulders, grooves, and other critical areas.
- Finishing: define the final diameter, flatness, roundness, and surface finish after coating and machining.
- Service environment: identify particles, fluids, temperature, contact pressure, and impact so the overlay is matched to actual use.
HVOF is not only a repair process. It can also be selected for new components where a dense, wear-resistant barrier is needed. The final recommendation should still be based on tested requirements and part geometry, not on process popularity alone.
Matching industrial coatings to manufacturing applications
Different manufacturing operations expose surfaces to different combinations of friction, pressure, temperature, contamination, and material transfer. The following examples are starting points for an engineering discussion, not guarantees of a particular coating result.
Stamping and forming
Stamping dies can experience galling, pickup, abrasive wear, and loss of edge definition. A PVD or DLC solution may be considered for draw beads, radii, punches, and other surfaces where lower friction and reduced adhesion are important. Edge condition, steel grade, forming lubricant, and the material being formed all affect the result.
Injection molding and plastic processing
Mold cavities, cores, shutoffs, gates, and runners may need improved release or resistance to abrasive fillers. Thin films can be evaluated where dimensional control is critical. Surface texture, venting, polishing, resin additives, and masking must be reviewed together because a coating cannot compensate for poor mold geometry or inadequate preparation.
Machining and cutting
Cutting tools are exposed to heat, abrasion, adhesion, and chip-flow conditions that change with the workpiece material and cutting parameters. PVD coating services may support edge retention and reduce built-up edge when the coating, edge preparation, tool substrate, and cutting strategy are compatible.
Die casting and extrusion
Dies, pins, sleeves, and related surfaces can face soldering, washout, thermal cycling, and erosion. The correct treatment may combine a thick overlay on a wear surface with a thin film on a precision feature. Thermal history, dimensional allowance, and post-coating finishing need to be defined before processing.
Shafts, sleeves, and industrial components
Rotating components may require an overlay that resists particle erosion or restores a worn diameter. Thermospray or pulsed HVOF can be considered when the project needs substantial buildup and controlled finishing. The supplier should understand the load, speed, counterface, fluid, contamination, and inspection requirements.
This high-performance coatings overview provides additional context on how engineered surface treatments can be applied across demanding industrial environments.
How to evaluate industrial coatings services
A capable supplier should be able to discuss your failure mode in measurable terms and explain how its process controls address it. Look beyond a list of coating names. Ask how the company handles preparation, masking, fixturing, inspection, rework, traceability, and scale-up.
Capability and process fit
Confirm that the provider runs the process your geometry requires. PVD depends on chamber access, fixturing, and line-of-sight. HVOF and other thermal spray methods depend on spray angle, surface preparation, access, buildup allowance, and finishing. A supplier with both thin-film and thick-overlay options may be able to assess mixed requirements more efficiently.
Preparation and finishing
In-house blasting, microblasting, degreasing, stripping, polishing, and lapping can reduce handoffs and make process responsibility clearer. Ask which steps are performed internally, how critical surfaces are masked, and how the original dimensions are protected during stripping or refurbishment.
Quality and documentation
Agree on the measurements that matter before the first production run. Depending on the application, these may include coating thickness, uniformity, adhesion, hardness, surface roughness, dimensions, and visual inspection. Documentation should identify the part, process route, inspection results, and any approved deviations.
Sputtek states that it operates under ISO 9001:2015 and Nuclear N299.3 quality requirements. It also identifies SPUN 2,000 and SPUN 4,000 PVD systems with capacities of up to 1,200 kg per cycle and 3,000 kg per cycle respectively. Confirm current equipment availability, qualification requirements, and the exact capacity relevant to your part mix during supplier review.
For a local overview of PVD applications and terminology, see the Woodbridge vapor-deposition coating guide. A supplier discussion should end with a testable process plan, not only a recommendation to “try” a coating.
Preparation, masking, and quality control
Preparation is often the difference between a coating that looks acceptable and one that performs consistently. Oils, residues, oxides, embedded media, and unsuitable surface texture can interfere with adhesion. The treatment must also respect the substrate: aggressive preparation or uncontrolled stripping can change dimensions or damage a critical edge.
Prepare the part
Start with a clean drawing or inspection record showing datums, fits, sealing faces, threads, edges, and surfaces that must remain free of coating. Identify prior coatings, heat treatment, contamination, and any known damage. For a failed part, photographs and operating information can help distinguish coating wear from substrate or process problems.
Control masking and fixturing
Masking protects holes, datums, bearing fits, and other restricted areas. Fixturing must expose the working surfaces consistently without creating shadowing, movement, or contact damage. The design should reflect whether the part is going into a vacuum chamber or requires a controlled thermal-spray path.
Verify the finished surface
Inspection should be connected to function. Measure dimensions where fit matters, surface finish where release or sealing matters, and coating properties where wear or adhesion matters. Use representative locations and agree on acceptance criteria before processing so a result is not judged only by appearance.
When a project moves from trial to production, preserve the approved preparation route, fixturing arrangement, coating recipe, finishing method, and inspection plan. That process record makes it easier to investigate changes in tool life or surface behavior later.
Planning industrial coatings services in Woodbridge
For a Woodbridge manufacturer, local planning can simplify technical communication, part movement, and trial iterations. Sputtek lists its facility at 110 Sharer Rd in Woodbridge, Ontario, within the Greater Toronto Area. The relevant advantage is not simply proximity; it is the ability to coordinate engineering review, preparation, coating, finishing, and quality documentation through one local point of contact.
Before sending parts, prepare a concise package containing the drawing, substrate and heat-treatment information, service conditions, failure photographs, production volume, previous coating history, and required turnaround. Include the surfaces that must not be coated and identify whether the part is a prototype, repair, or repeat production item.
Local access can also make controlled trials easier. A team may begin with representative parts, compare a small number of coating routes, inspect the results, and then update the process before committing a larger batch. That approach is more informative than changing several variables at once.
For additional perspective on thin films in the area, review this Woodbridge thin-film coating overview. The final selection should still be based on the part’s operating conditions and measured performance rather than location alone.
A practical project checklist
Use the following sequence to make a coating project easier to scope and validate:
- Describe the failure: record where wear, sticking, corrosion, erosion, cracking, or material transfer occurs.
- Define the duty: provide loads, speed, temperature, contact materials, fluids, particles, cycle count, and maintenance history.
- Separate critical surfaces: mark coated areas, restricted areas, datums, fits, edges, and finish requirements on the drawing.
- Choose the process family: evaluate PVD/DLC for precision and friction problems; evaluate Thermospray/HVOF for thick wear or rebuild requirements.
- Agree on preparation: specify cleaning, roughening, masking, fixturing, and any stripping or refurbishment route.
- Set acceptance criteria: define dimensions, thickness, adhesion, hardness, finish, inspection points, and documentation.
- Run a controlled trial: change as few variables as possible and compare the coated part under representative conditions.
- Document the production route: retain the approved recipe and inspection record before scaling volume.
This sequence gives engineering, purchasing, operations, and quality teams a shared basis for comparing industrial coatings services. It also helps prevent a common mistake: selecting a coating from a catalogue before defining what the surface must do.
Frequently asked questions
What is the difference between PVD/DLC and HVOF coating?
PVD and DLC are thin films used to modify friction, hardness, release, or adhesion while preserving close geometry. HVOF is a thermal-spray process that builds a thicker, dense overlay for abrasion, erosion, impact, or dimensional recovery. The correct choice depends on the part and failure mechanism.
How do I choose an industrial coating for a tool or component?
Start by identifying the dominant failure and the operating conditions that produce it. Then compare substrate compatibility, geometry, coating thickness, preparation, finishing, and inspection requirements with a qualified supplier. A coating recommendation should lead to a measurable trial plan.
Can coated tools be stripped and recoated?
Many tools and components can be stripped and recoated when the method is controlled for the substrate, dimensions, and surface condition. The supplier should confirm that stripping will not damage edges, fits, or critical surfaces. Recoating should include inspection and preparation rather than simply repeating the original deposition cycle.
Do industrial coatings change part tolerances?
Any coating can affect a tolerance, but the extent depends on the process and layer thickness. PVD and DLC add a relatively thin film, while Thermospray and HVOF require a planned buildup and usually post-coating finishing. Provide the drawing and critical dimensions before the process is selected.
Discuss your industrial coatings application
Industrial coatings services work best when the coating, preparation, finishing, and inspection plan are designed around the actual failure. Share a representative part, drawing, operating conditions, and failure evidence with Sputtek to discuss whether PVD, DLC, Thermospray, pulsed HVOF, or another surface route fits your production needs.